In large-scale commercial and multi-family residential procurement, lighting components are often treated as minor budget lines. However, they frequently become the source of the most expensive, open-ended remediation costs on-site.
Many international procurement managers sign off on shop drawings focusing solely on aesthetics, raw lumen output, and wholesale pricing. Yet, the high-duty cycles of commercial properties, combined with rigorous overseas building codes, will quickly expose any compromise in manufacturing quality.
Rather than rehashing standard laboratory metrics, this article reviews several practical technical oversights we have encountered during international project handovers and evaluates their financial impact on developers.
1. The Mockup Room Discrepancy: How Low-CRI Chips Compromise Premium Finishes
This is a frequent cost-overrun issue in high-end hospitality projects. In a past project, the procurement team attempted to optimize profit margins by selecting a commercial downlight vendor whose unit pricing was 15% below market average.
The supplier provided standard lumen verifications, but during the final mockup room inspection, the architectural design team rejected the installation entirely.
Under the low-end Ra 80 chips provided, the high-grade natural marble wall claddings appeared muted and gray. The custom wood veneers lost their warm undertones, resulting in a finish that fell significantly short of the project’s marketing renderings. The design team requested an immediate re-evaluation of the lighting package. Following rigorous on-site mockup testing, the developer decided to replace the fixtures across all primary display areas and guest suites, upgrading to custom arrays utilizing chips specified at Ra≥90 and a red saturation index of R9≥80.
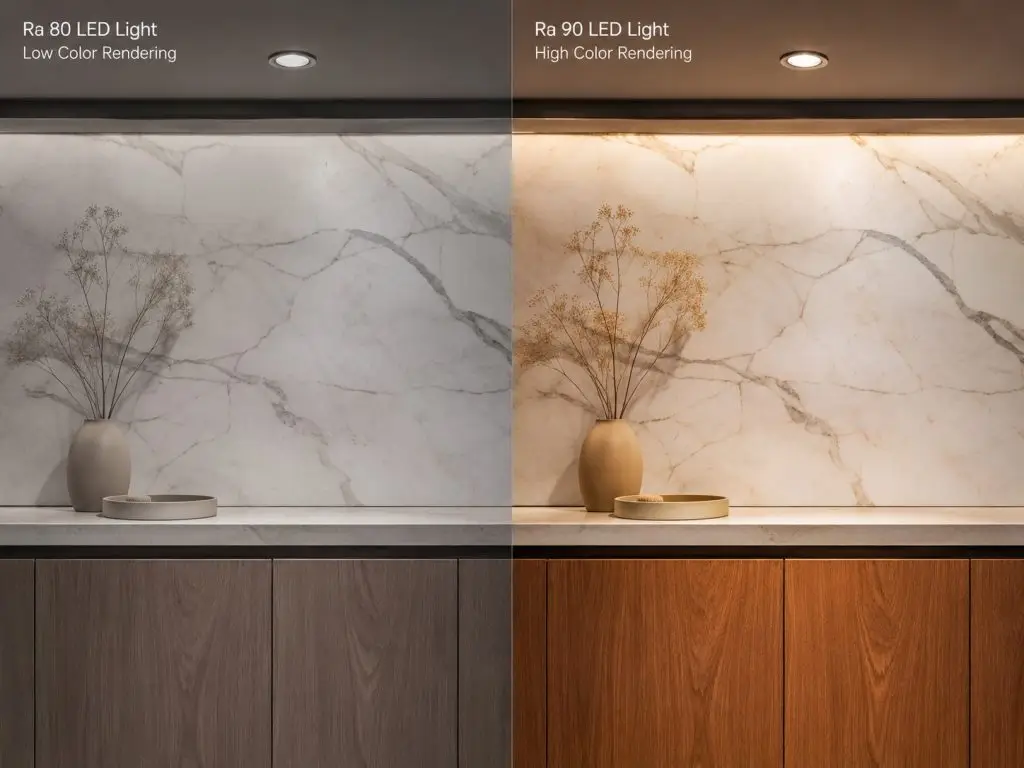
On-Site Takeaway: For luxury retail, hospitality, and high-end residential spaces, color rendering indexes are non-negotiable architectural requirements. Standard engineering fixtures prioritize lumens over spectral completeness to save costs. Locking in high-performance spectrum parameters during the initial scheduling phase is critical to avoiding secondary installation labor costs overseas.
2. Material Degradation in Humid Climates: The Cost of Substituted Diffusers
A regional developer managing coastal residential builds recently approached our team to engineer a complete lighting replacement package for a two-year-old multi-family complex. The linear LED diffusers throughout the public corridors had severely yellowed and embrittled, resulting in multiple tenant complaints.
While the site team initially assumed they had received a defective batch of acrylic, we subsequently commissioned a third-party material testing agency to analyze the degraded polymers. The results revealed a standard industry compromise: the factory had substituted the specified PMMA (Acrylic) with a cheap, non-UV-stabilized plastic blend to secure a low-bid contract.
Low-tier plastics lack the molecular stability required to withstand the continuous thermal output of high-power LED boards paired with external UV exposure. Within 18 to 24 months, these materials undergo accelerated photo-oxidation, turning brittle and yellow.
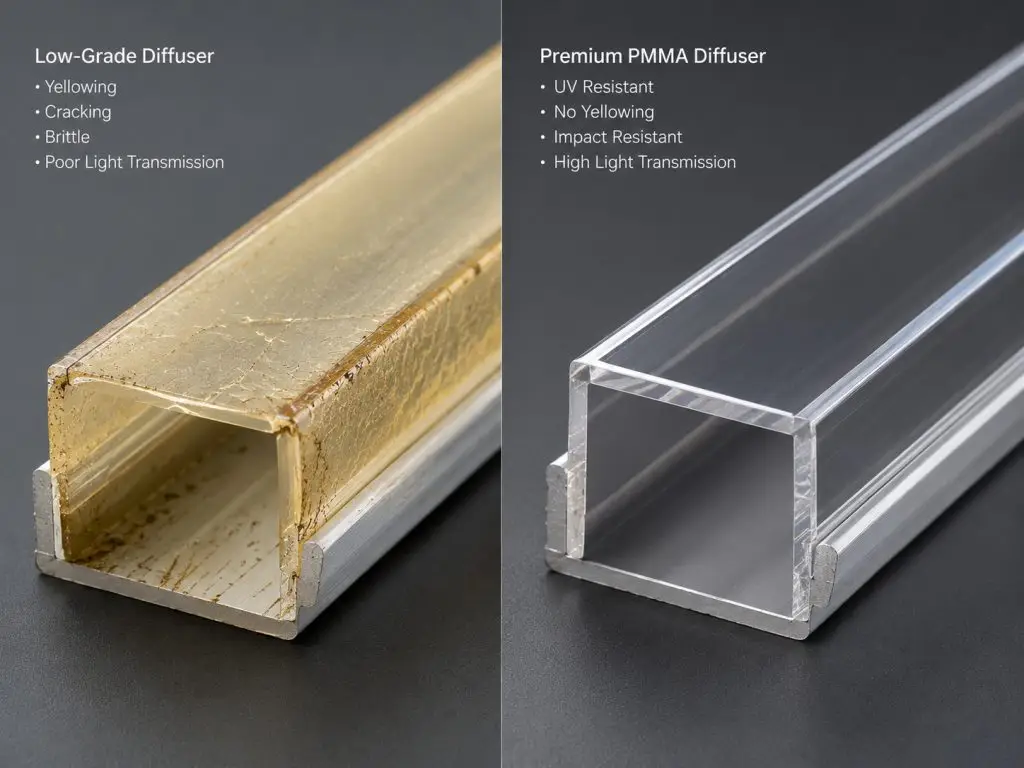
Material Selection Standard: For bulk export contracts—particularly into high-UV or high-humidity regions like the Middle East or coastal Australia—procurement specifications must explicitly mandate PMMA or high-grade Polycarbonate (PC) for all optical extrusions. PMMA maintains a 92% light transmittance rating over time. For high-volume freight safety, an intermediate alternative like MS polymer can balance impact resistance and surface hardness, but baseline PVC or low-end plastics should be strictly banned from commercial specifications.
3. Compliance and Customs Holds: The Regulatory Risk of Uncertified Drivers
This operational failure stems from a lack of supply chain auditing regarding international customs regulations. During a multi-family residential project in North America, the design required an advanced dimming infrastructure, utilizing 0-10V and DALI protocols to enable automated, 24-hour circadian rhythm control.
The system design was correct, but the procurement team compromised on the component level. To minimize total contract costs, they sourced the dimming drivers from a regional domestic factory that lacked international compliance experience, failing to verify the necessary certification marks for the destination country.
When the bulk cargo arrived at the port of entry, US Customs detained the entire container because the electronic drivers lacked valid UL certification and verified electrical safety documentation.
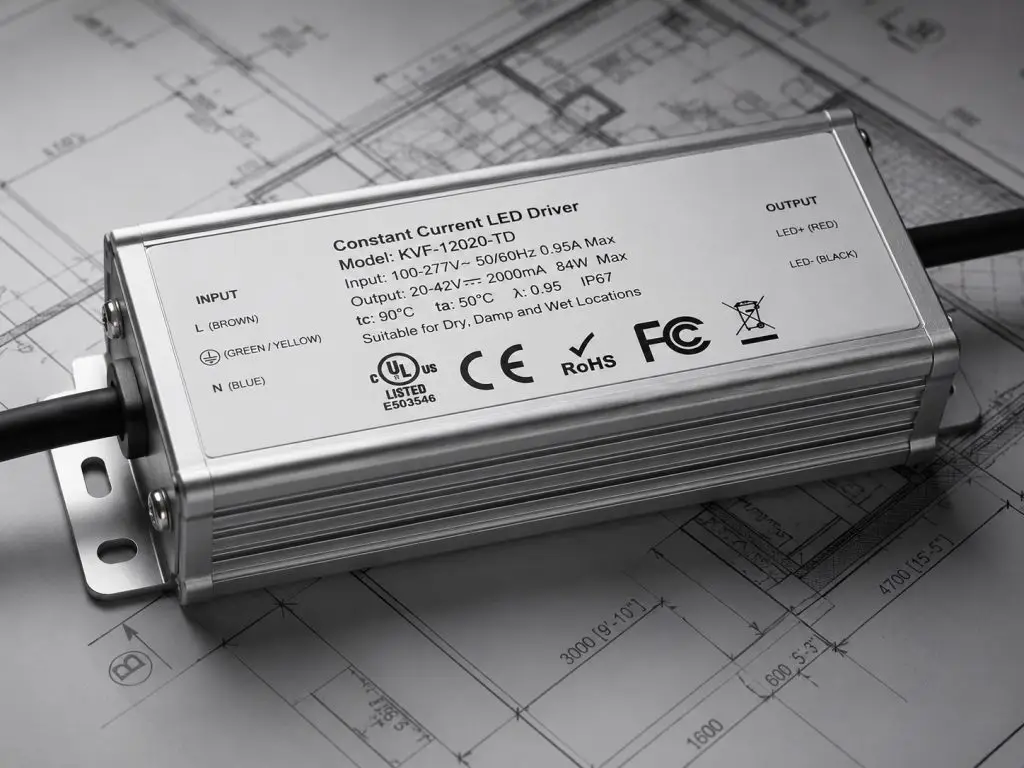
On-Site Takeaway: Every mass-production contract destined for international markets must undergo a rigorous regulatory audit before manufacturing begins. Uncertified electrical equipment is subject to immediate border seizures or severe port demurrage fines. Furthermore, local commercial building inspectors, fire marshals, and insurance underwriters will deny occupancy permits to properties utilizing unlisted fixtures, completely erasing any initial product cost savings.
4. Spatial Clashes: Plenum Depth vs. Deep-Cone Anti-Glare Architecture
The modern shift toward minimal architectural lighting has made the integration of deep-cone recessed spotlights standard practice. To achieve effective glare control and clean visual ceilings, architectural specifications regularly require fixtures with a cutoff angle of 45° or higher.
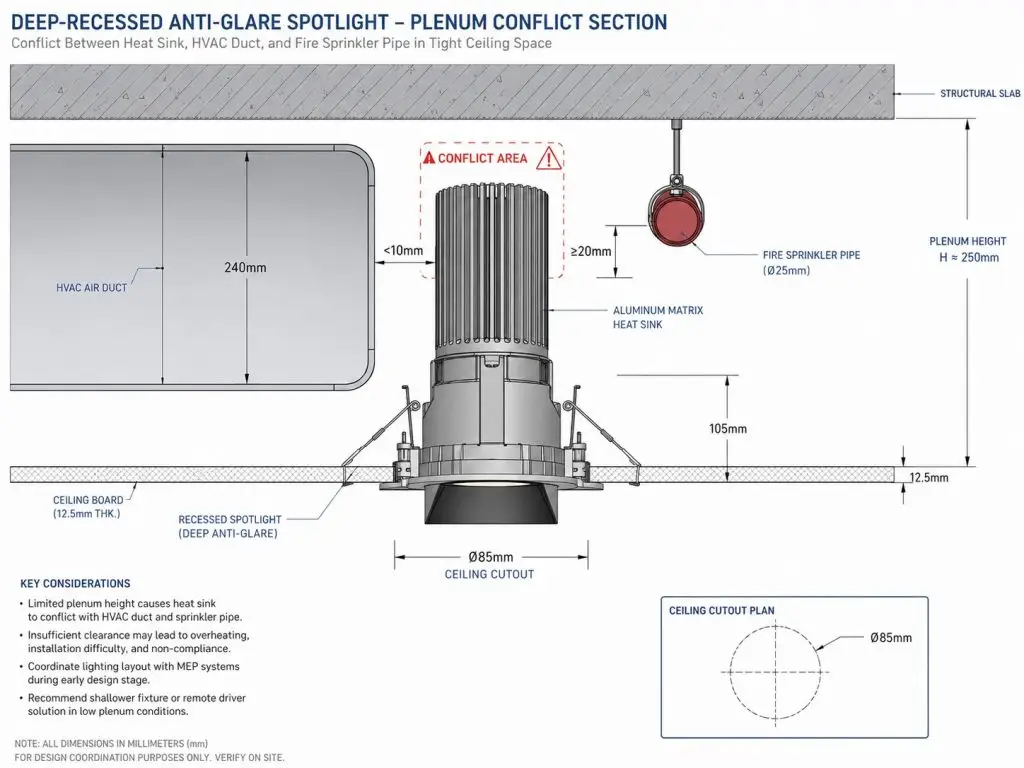
However, deep-cone anti-glare physics dictate that the fixture housing and its associated heat sink profile must be significantly taller than a standard flat panel downlight.
During the coordination phase of a recent hotel project, our engineering team successfully intercepted a major spatial conflict before mass production commenced. The contractors had pre-drilled the ceilings based on 2D layouts but overlooked the highly congested plenum space, which was packed with HVAC ductwork, fire sprinkler mains, and structural framing. Our pre-production audit revealed that the heavy aluminum matrix heat sinks of the specified deep-cone spotlights would physically collide with the fire mains, completely preventing the spring clips from engaging.
Technical Solutions & Procurement Strategy
Managing these complex physical and regulatory variables requires a supply chain partner capable of moving beyond simple order fulfillment into structured, upfront risk management.
At George Group, our engineering and manufacturing workflows were built specifically to de-risk these international contracts. Before initiating mass production from raw architectural schedules, our technical team conducts a mandatory pre-production review. We verify destination electrical codes (ensuring full UL, CE, or RoHS driver compliance), cross-check material formulations for regional climate resilience, and model plenum clearances against structural MEP (Mechanical, Electrical, Plumbing) drawings.
If a spatial clash is detected—such as a deep-cone fixture hitting a structural beam—our lines adapt through flexible manufacturing. We re-engineer the housing into an asymmetric, low-profile offset heat sink or utilize remote driver configurations to preserve the 45° anti-glare profile. Furthermore, every production batch undergoes mandatory full-load burn-in and electrical stability testing prior to crating, ensuring consistent operational reliability upon field arrival.
For international developers and construction managers, mitigating procurement risk is ultimately a matter of choosing a manufacturing partner that understands how a fixture performs not just on a balance sheet, but during hand-over inspections and over years of live operations.